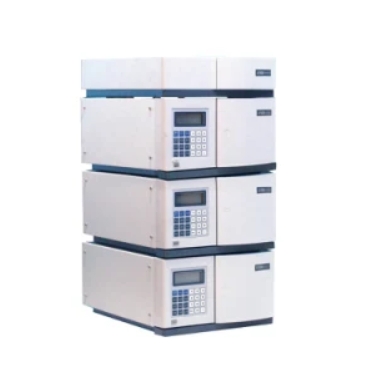
The Wincom LC1620B HPLC is an advanced, high-performance liquid chromatography system engineered for higher precision, automated workflows, and complex analytical separations. This complete configuration features an upgraded high-pressure solvent delivery pump, an ultra-low noise UV-Vis detector, a high-accuracy manual injector (or optional autosampler support), and a premium separation column. With enhanced electronic control and improved baseline stability, the LC1620B is ideal for high-throughput testing in pharmaceuticals, food security, environmental protection, and chemical research.
System Configuration and Specifications
1. High-Pressure Constant-Flow Pump (LC1620B Series)
Flow Rate Range: 0.001 mL per minute to 10.000 mL per minute
Maximum Operating Pressure: 42 Megapascals (MPa) (with upgraded pressure pulse damping)
Flow Rate Precision: Relative Standard Deviation (RSD) less than 0.06 percent
Pump Design: Advanced dual-piston reciprocating pump with electronic flow compensation for ultra-smooth solvent delivery.
2. UV-Vis Detector
Wavelength Range: 190 nm to 700 nm
Wavelength Accuracy: +/- 1 nm
Baseline Noise: Less than or equal to 0.5 x 10^-5 Absorbance units (Lower noise floor than previous models)
Baseline Drift: Less than or equal to 1 x 10^-4 Absorbance units per hour
Optical System: Upgraded dual-beam holographic optical path for superior stability.
3. Manual Injector
Injector Type: Authentic Rheodyne 7725i manual injection valve with built-in position sensor
Loop Volume: Standard 20 microliter sample loop (customizable from 5 to 500 microliters)
Signal Trigger: Automatic signal synchronization with the software workstation upon sample injection.
4. Chromatography Column and Oven
Column Type: Premium C18 Reversed-Phase Column (5 micrometer, 4.6 mm internal diameter x 250 mm length)
Column Oven Temperature Range: Ambient temperature plus 5 degrees Celsius to 80 degrees Celsius
Temperature Control Accuracy: +/- 0.1 degrees Celsius (Supports intelligent temperature programming)
Key Features
Enhanced Baseline Stability: The LC1620B system introduces a redesigned electronic shielding and optical path that significantly cuts down background noise, allowing the detection of trace components.
Auto-Protection System: Features intelligent over-pressure limits, low-pressure leakage protection, and automated solvent level warning indicators to prevent dry running.
Precise Gradient Elution: Supports high-pressure binary or low-pressure quaternary gradient configurations, enabling fast separation of highly complex samples.
Intelligent Data Software: Accompanied by user-friendly chromatography software that handles instrument control, peak integration, quantitative report generation, and data security compliance.
Primary Applications
Pharmaceuticals and Biotechnology: Content uniformity testing, drug stability assays, impurity profiling, and separation of active pharmaceutical ingredients (APIs).
Food and Consumer Safety: Rigorous testing for illegal food dyes, chemical preservatives, microcystins, and residual veterinary drugs in meats.
Environmental Monitoring: Detection of phenols, polycyclic aromatic hydrocarbons (PAHs), and modern chemical pollutants in industrial wastewater.
Cosmetics and Chemical Industry: Analyzing raw chemical ingredients, essential oils, organic pigments, and personal care formulations.
Reviews
There are no reviews yet.